



Product Description
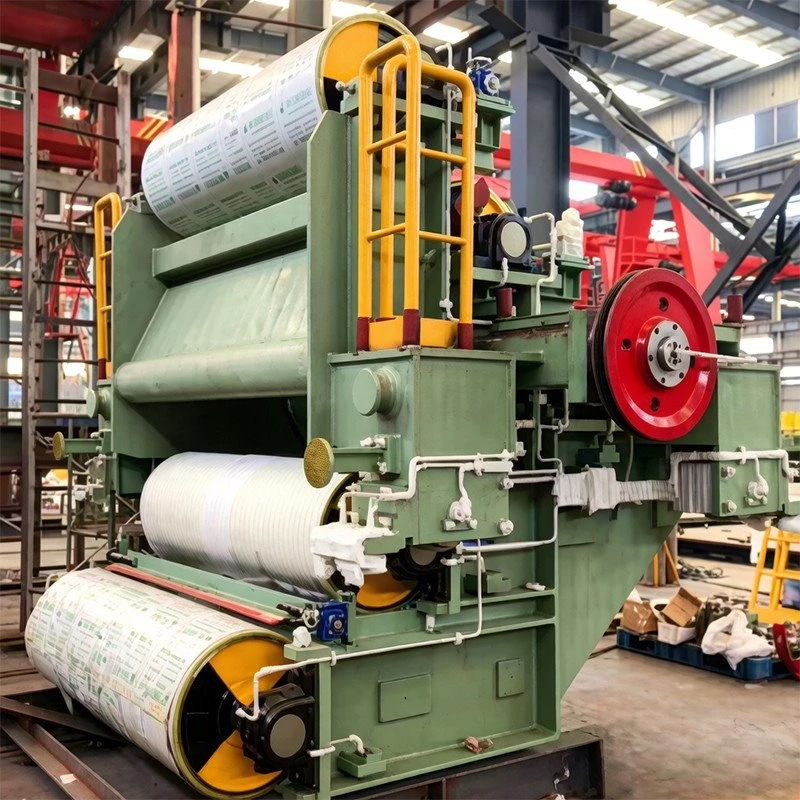
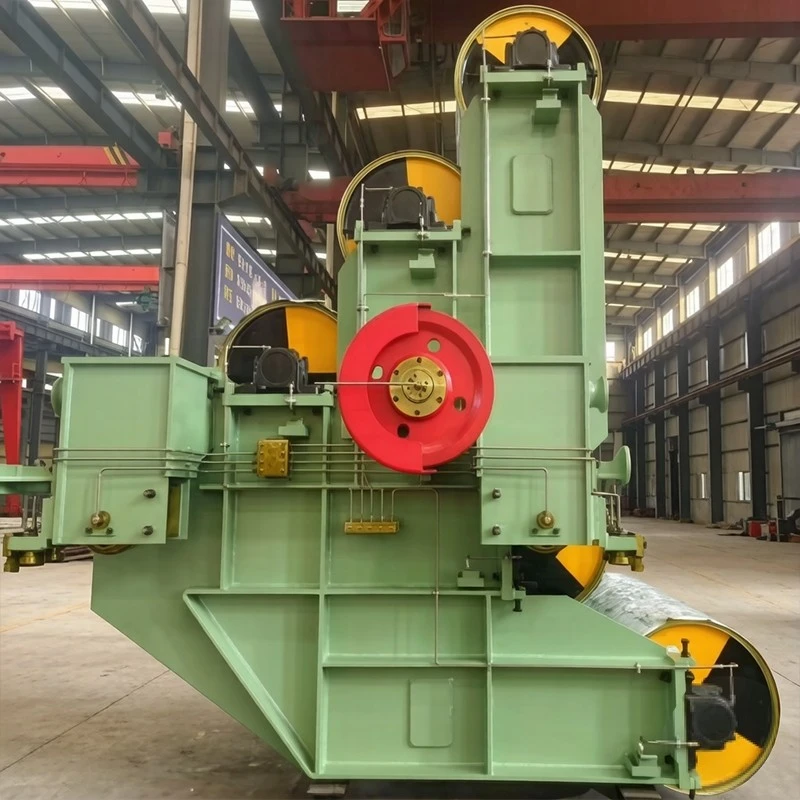
Engineered and built at our specialized metallurgical machinery complex in Jingjiang, our Vertical Accumulator Looper is a heavy-duty strip accumulator tower engineered for continuous strip processing lines-such as pickling lines, continuous galvanizing lines (CGL), and continuous annealing lines (CAL). Leveraging 26 years of heavy equipment manufacturing expertise and serving leading steel producers including Baowu, Nangang, and POSCO, we manufacture each Vertical Accumulator Looper with precision-machined vertical tower columns, a counterweighted traveling looper carriage, and multiple fixed and movable roll sets. By accumulating or discharging strip during entry-end coil welding or exit-end coil unloading, this high-capacity Vertical Accumulator Looper guarantees uninterrupted processing through central furnace and coating sections, providing cold-strip producers with a reliable buffering asset built for continuous high-speed production.
Applications
Continuous Galvanizing Lines (CGL): Buffering strip at entry and exit ends to maintain constant speed through the zinc pot and annealing furnace.
Continuous Pickling Lines (CPL): Storing strip during tail joining to ensure continuous, steady speed through acid tanks.
Continuous Annealing Lines (CAL): Preventing furnace thermal shocks by ensuring uninterrupted strip travel during coil changes.
Color Coating Lines (CCL): Maintaining constant web speed through paint coaters and curing ovens.

Technical Specifications
|
Design Standards |
Cold Strip Processing Machinery Standards, ISO 9001, JB/T 5000 |
|
Structural Configuration |
Vertical multi-column tower with top/bottom fixed roll banks and a traveling middle carriage |
|
Strip Storage Capacity |
100 m to 600 m of accumulated strip length |
|
Storage Duration |
60 to 180 seconds at full process speed |
|
Strip Width Capacity |
600 mm to 2,200 mm; Strip thickness: 0.2 mm to 4.5 mm |
|
Line Speed |
Process speed up to 350 m/min; Entry/exit carriage acceleration up to 600 m/min |
|
Traveling Carriage Drive |
AC vector motor with variable-frequency drive, winch drum, and heavy wire-rope reeving (or hydraulic cylinder drive) |
|
Guide System |
Machined vertical guide rails with heavy roller guide assemblies to eliminate carriage skewing |
|
Roll Surfaces |
Rubber/polyurethane covers, chrome plating, or tungsten carbide coatings |
Customization Capabilities
Storage Capacity Optimization: Tailoring tower heights, column cross-sections, and strand reeving passes (typically 8 to 24 strands) to match line speed and coil weld cycle times.
Carriage Anti-Skewing Systems: Mechanical rack-and-pinion synchronizers or dual-encoder digital skew controls to keep the traveling carriage level.
Integrated Strip Steering Rolls: Intermediate steering roll units installed within the looper tower to maintain strip tracking across tall accumulators.
Controlled Strip Tension Profiles: Low-inertia carriage drives and counterweight systems that maintain consistent strip tension during rapid carriage acceleration and deceleration.
Zero MOQ Restriction: Custom engineered for accumulator retrofits or delivered as complete processing-line packages.
Quality Control
Manufacturing Accreditations: ISO 9001:2015, ISO 14001:2015, and ISO 3834-2 welding quality management.
Full Process QR Code Traceability: Structural columns, winch drums, wire rope sheaves, traveling carriages, and roll assemblies carry individual QR codes linked to certified test records.
Tower Alignment & Geometry Checks: Workshop trial assembly of tower sections, guide rail alignments (straightness within 1 mm/10 m), and carriage travel verification.
Dynamic Balancing: All looper rolls undergo dynamic balancing to ISO 1940 Grade G2.5 to prevent chatter marks on strip.
Heavy Ocean Packaging: Segmented tower columns with structural bracing, greased machined ways, weather-sealed electrical/hydraulic skids, and crated roll assemblies.
FAQ
Q: How do you prevent strip wandering inside tall vertical accumulator towers?
A: We machine tower guide rails to strict tolerances to eliminate carriage tilt, dynamically balance all looper rolls, and integrate intermediate steering guide units within the strand array to maintain centerline tracking.
Q: What is the typical manufacturing lead time for a complete vertical looper?
A: Tower fabrication, carriage machining, and shop trial assembly typically require 4 to 6 months from engineering drawing approval to factory dispatch.
Q: What warranty coverage do you provide?
A: We provide an 18-month warranty from site arrival or 12 months from commercial operation (whichever occurs first).
Q: What payment terms and currencies do you support?
A: Standard commercial terms are 30% advance deposit, 40% manufacturing milestone payment, and 30% balance prior to export shipment, payable in USD, EUR, or RMB.
Hot Tags: vertical accumulator looper, China vertical accumulator looper manufacturers, suppliers, factory, Automatic Cable Coiler, Belt Wrapping Machine, Furnace Roller, Horizontal looper, Looper Unit Equipment, Self lubricating furnace roller


