

Product Description
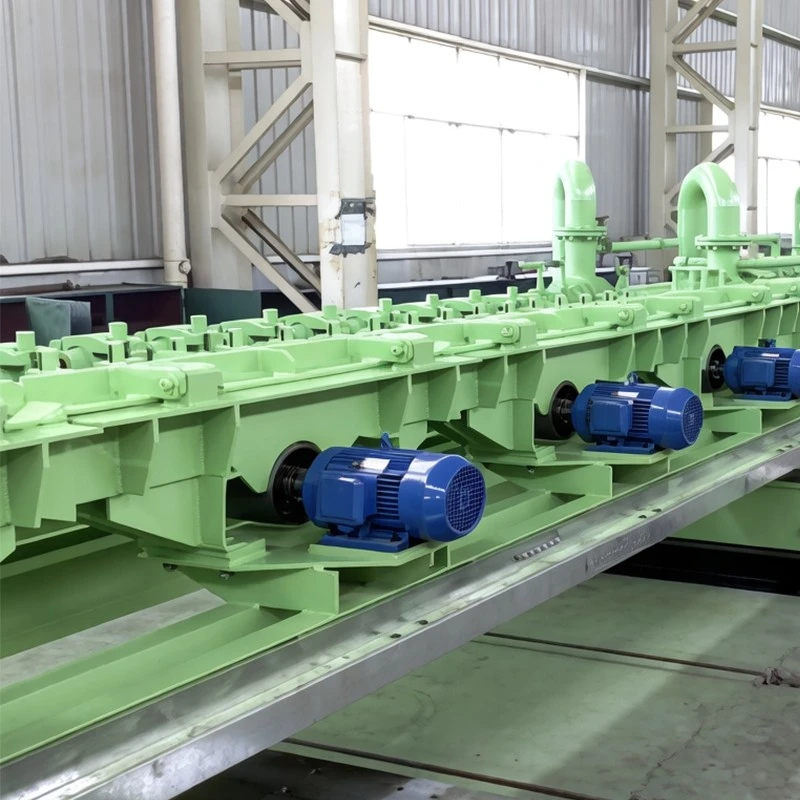
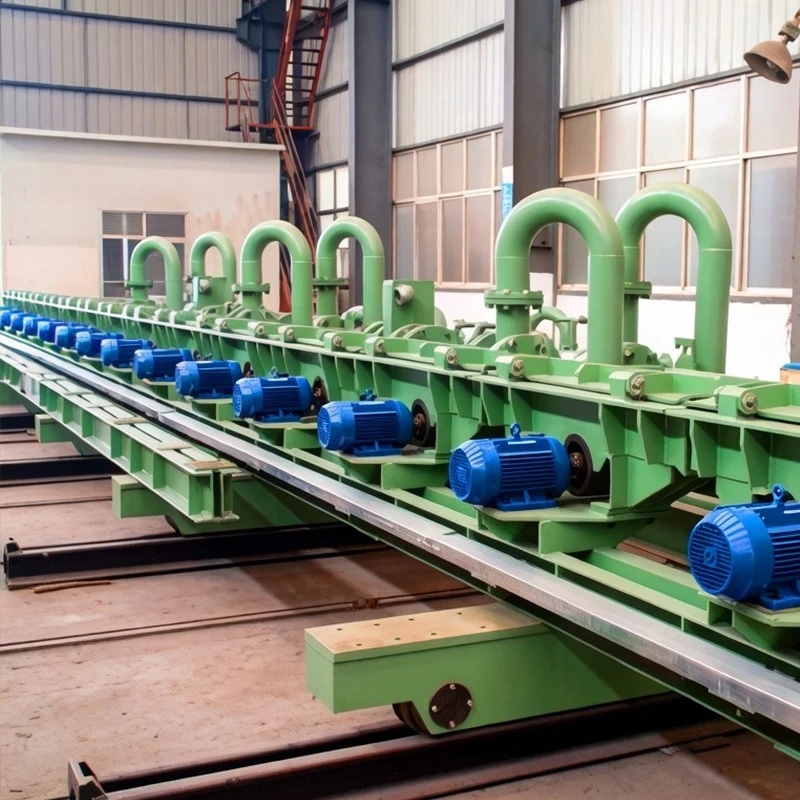
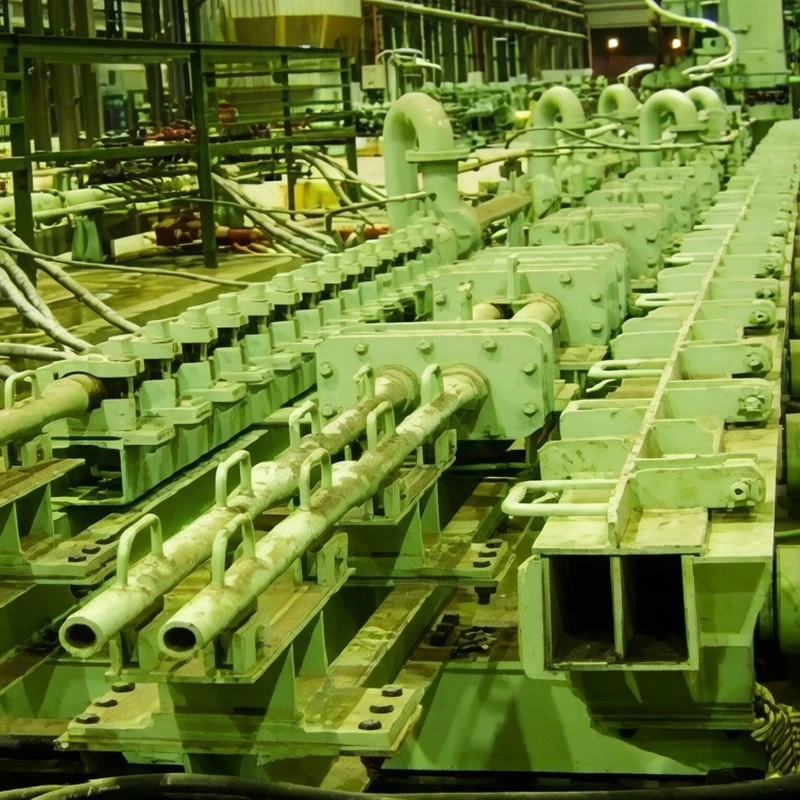
Adding micro-alloys like vanadium or niobium to a heat just to meet Grade 60 or seismic yield specs adds thousands of dollars per shift to melt shop operating costs. We build the Rebar Thermex Cooling System at our Jingjiang manufacturing facility specifically to eliminate that alloy surcharge through controlled water quenching and self-tempering right behind the finishing stands. Backed by 26 years of heavy mill-equipment fabrication-and decades of supplying rolling hardware to groups like Baowu, Shagang, and POSCO-our fabrication crew puts together each Rebar Thermex Cooling System using heavy motorized rail skids, CNC-drilled stainless spray manifolds, and quick-lift split covers. It catches hot bar running between 10 and 45 m/s at around 1,050°C, strips the steam barrier with balanced water jets to freeze the outer skin into hard martensite, and lets core heat migrate back out on the cooling bed to temper that rim into ductile sorbite. Every manifold block is 100% hydro-tested in our yard and backed by full heat-number QR tracking, giving bar mills a reliable tool to roll weldable high-strength rebar with minimal alloy additions.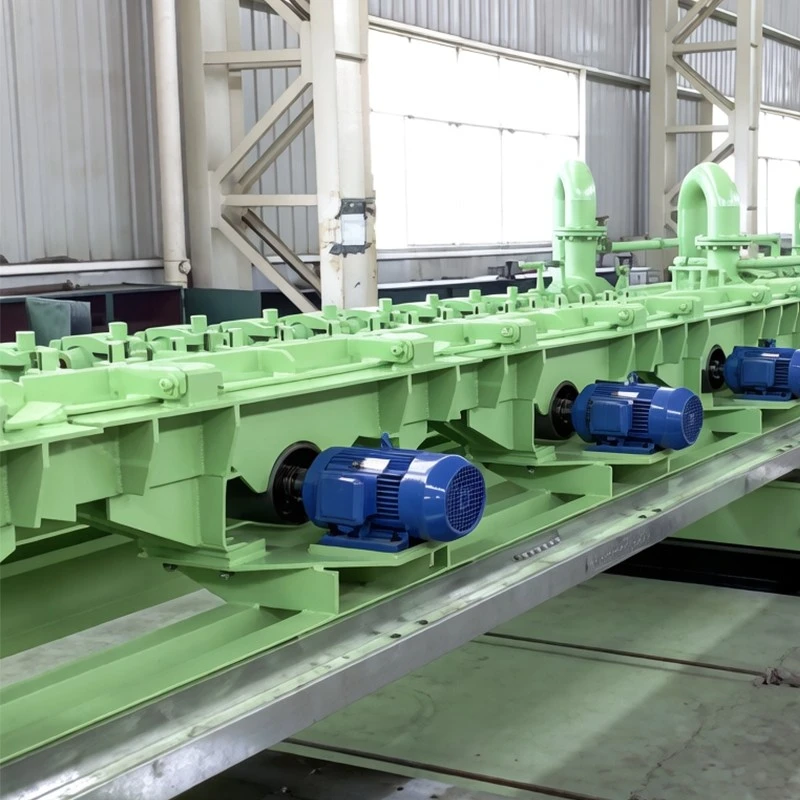
Applications
Seismic-Grade Concrete Reinforcing Bar: Rolling weldable rebars (HRB400E, HRB500E, BS 4449 B500B, CS2:2012, and ASTM A615 Gr 60/75/80) without failing 180° cold bend tests.
Slit-Rolling Operations: Multi-line bar setups (2-strand, 3-strand, or 4-strand slitting) where each strand needs its own calibrated water jacket.
Melt Shop Alloy-Reduction Projects: Dropping expensive ferro-alloys out of the ladle metallurgy furnace while keeping rebar yield strengths comfortably above design minimums.
Line Revamps and Bottle-Neck Clearing: Swapping out leaky, stationary cooling troughs for a traversable skid that can be rolled off-line when running plain round bar.
Technical Specifications
|
Applicable Bar Sizes |
Ø10 mm to Ø50 mm (single-strand and slit lines) |
|
Mill Delivery Speeds |
6 m/s on heavy bar up to 45 m/s on high-speed finishing blocks |
|
Dynamic Operating Water Pressure |
0.8 MPa to 2.5 MPa |
|
Typical Cooling Water Demand |
300 to 1,800 m³/h, depending on bar size and tonnage |
|
Bar Feed Temperature |
980°C–1,050°C right out of the final stand |
|
Cooling Bed Equalization Temperature |
580°C to 680°C |
|
Rim-to-Core Ratio |
Martensitic/tempered rim depth calibrated to 8%–12% of the bar radius |
|
Resulting Mechanical Values |
Yield strength 420–620+ MPa; Rm/ReL ≥ 1.25; Agt uniform elongation ≥ 9.5% |
|
Manifold Metallurgy |
304/316L stainless steel pipework with hardened tungsten carbide guide tips |
|
Design and Testing Codes |
ISO 9001:2015, GB/T 1499.2, mill mechanical equipment standards |
Customization Capabilities
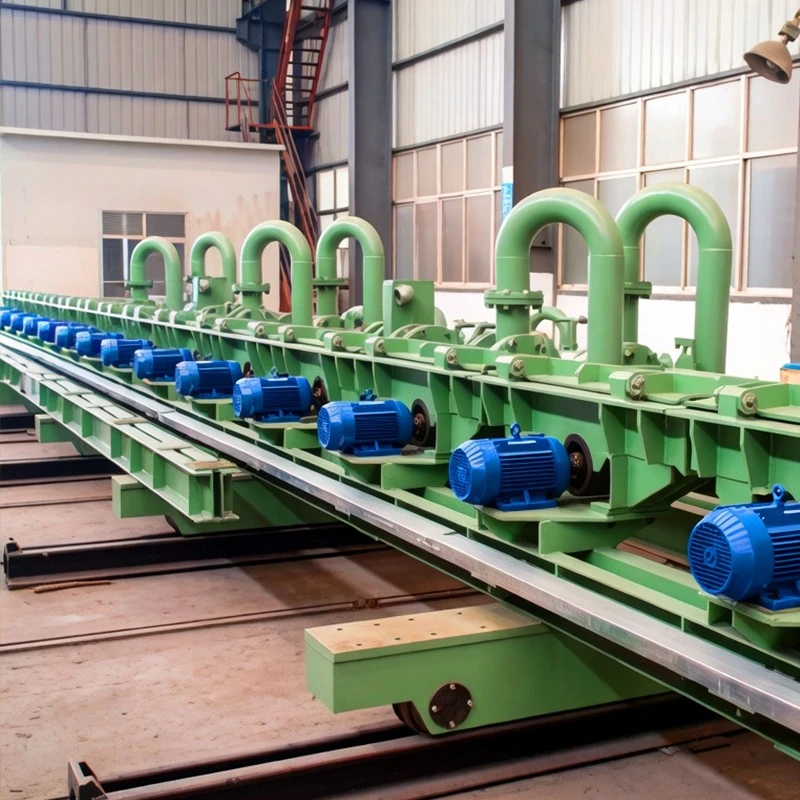
Motorized Shift-Out Rails: We mount the whole quench line on heavy floor tracks driven by an electric gearmotor. If you need to switch from rebar to merchant rounds, your operators can roll the quench box away and slide the bypass roller table into the mill center-line in under two minutes.
Strand-by-Strand Water Trim: On multi-strand slit mills, we split the water supply into dedicated headers with independent pressure gauges and manual or motorized trim valves so all strands exit at the same temperature.
Nozzle Angle Adjustments for Specific Water Heads: If your mill pump station runs low pressure, we recalculate the nozzle convergence angles and chamber lengths to make sure the water breaks through the steam film without needing new pump infrastructure.
Head-and-Tail Water Dump Controls: Pneumatic 3-way diverter valves that bypass the water flow for a fraction of a second as the bar nose and tail pass, preventing over-quenched "black ends" that snap shears.
Flexible Build Scope: Whether you need one replacement injector box for an emergency turnaround or a complete rail-mounted cooling section with local valving, we build it to order with no MOQ.
Quality Control
ASME and ISO Foundation: Built under our ISO 9001:2015, ISO 14001:2015, and ISO 3834-2 welding quality systems.
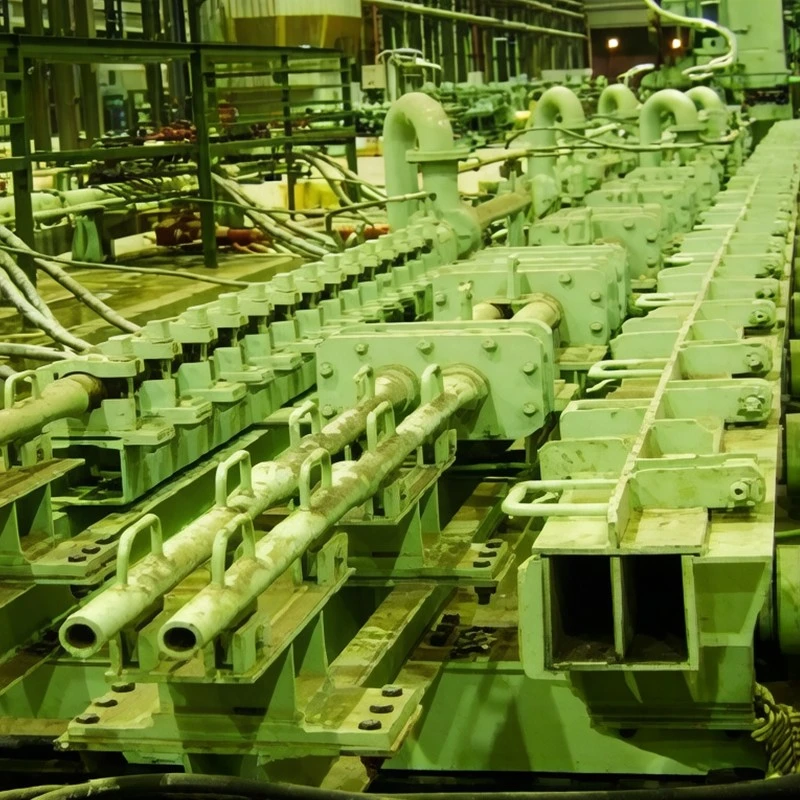
Individual QR Traceability: Every manifold pipe, nozzle body, welded frame beam, and valve assembly carries an engraved QR code linking back to raw material mill sheets and shop inspection sign-offs.
Hydrostatic Hold Testing: We fill every manifold with clean water, pump it to 1.5 times working pressure, hold it for 30 minutes to check for pinhole leaks, and verify that all nozzles spray with identical patterns.
Shop Trial Runs on Floor Tracks: We assemble the car, mount the cooling boxes, and run the motorized traversing carriage across its rails in our Jingjiang workshop to verify limit-switch stops and line-up accuracy before crating.
Export Breakbulk Packing: Welded structural steel cradles, grease-protected sliding ways, blind flanges on water inlets, and waterproof shrink wrap built for ocean shipment.
FAQ
Q: Why does this self-tempering process give high strength without making the steel brittle?
A: It comes down to how much heat you leave in the center of the bar. The water jets only freeze the outer 8% to 12% of the bar's cross section into hard martensite in the first couple of seconds. The center stays red-hot austenite above 850°C. As the rebar moves along the run-out table, that core heat soaks outward into the hardened shell, tempering it into tough sorbite while the middle cools into soft ferrite and pearlite. That is why the finished bar gives you high yield strength but still bends 180 degrees without snapping.
Q: What happens when there is a cobble inside the cooling line?
A: We design the top covers on heavy hinges connected to pneumatic cylinders. If a bar cobbles, the operator hits a switch at the desk to pop the covers open right away. Your crew can hook the scrap out with an overhead crane without having to unbolt any water pipes or dislodge the nozzles.
Q: How do we track manufacturing progress from abroad?
A: You get a dedicated project manager who sends weekly photo logs, weld inspection reports, and dimensional checks. We also set clear hold points for third-party inspectors-like BV, SGS, or your own team-to witness the hydro tests and check the rail alignment before anything gets packed.
Q: What are your commercial terms and delivery routines?
A: We ship under EXW or FOB terms out of our nearby Yangtze River terminal or Shanghai. Standard payment is 30% advance deposit, 40% after hydro-test inspection approval, and 30% balance before the ship sails. We accept USD, EUR, and RMB.
Hot Tags: rebar thermex cooling system, China rebar thermex cooling system manufacturers, suppliers, factory, water cooled backup roll, water cooled furnace chamber, water cooled heat shield, water cooled mill housing panel, water cooled reactor vessel, water cooled tundish equipment


