


Product Description
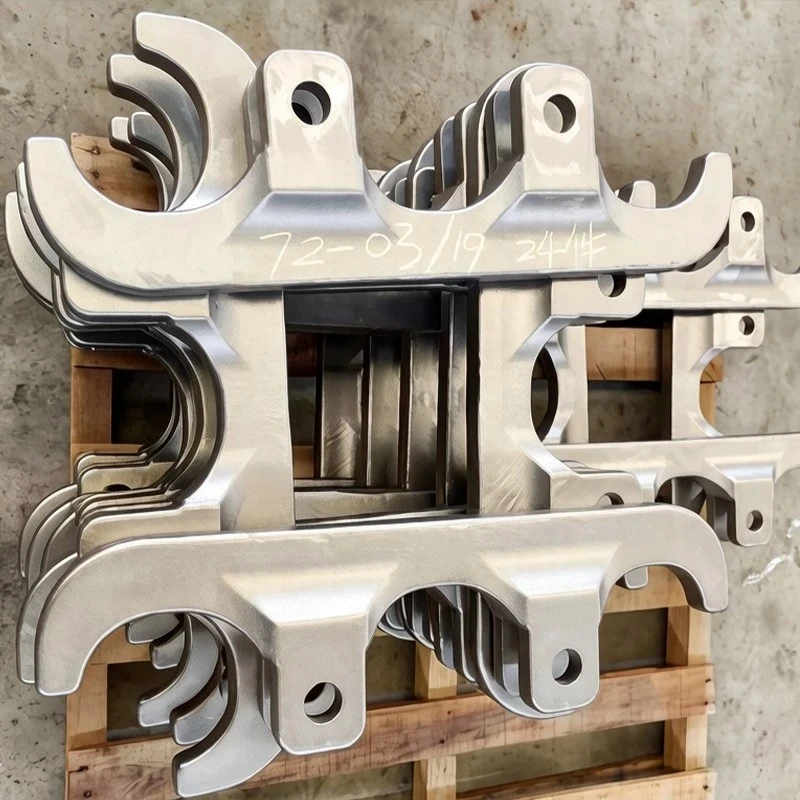
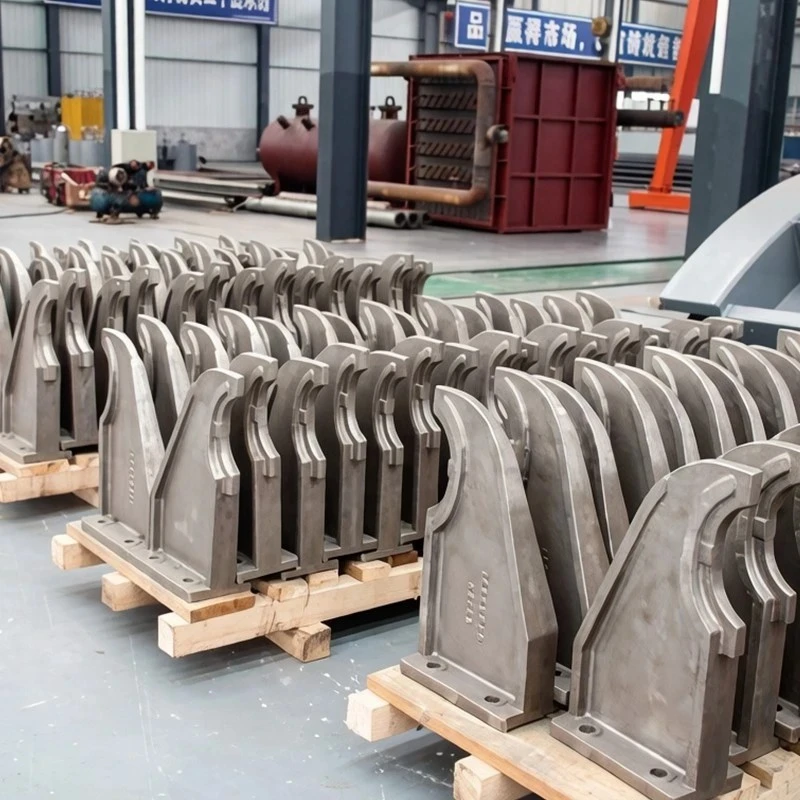
When radiant coil hangers seize or creep in a fired heater, tubes sag, refractory walls crack, and a forced turnaround is usually only months away. We cast and machine the Radiant Tube Support Hanger at our Jingjiang foundry specifically to take the thermal beating of radiant fireboxes while giving coils the freedom to expand. Backed by 26 years of heavy metallurgical casting experience-and routine supply to major refiners like Sinopec, CNPC, and international mills like POSCO-our foundry crew pours each Radiant Tube Support Hanger in high-nickel, high-chromium heat-resistant alloys like HK40, HP40, and IN-657. Engineered around API 560 clearances and cast with generous fillet radii, these hangers hold horizontal passes and suspend vertical coils in flue gas environments well above 870°C without binding or pulling down refractory anchors. Every batch is poured from spectro-checked heats, liquid-penetrant tested for shrinkage cracks, and stamped with a traceable QR code, giving furnace builders and maintenance crews a dependable casting that can be serviced without torching process tubes.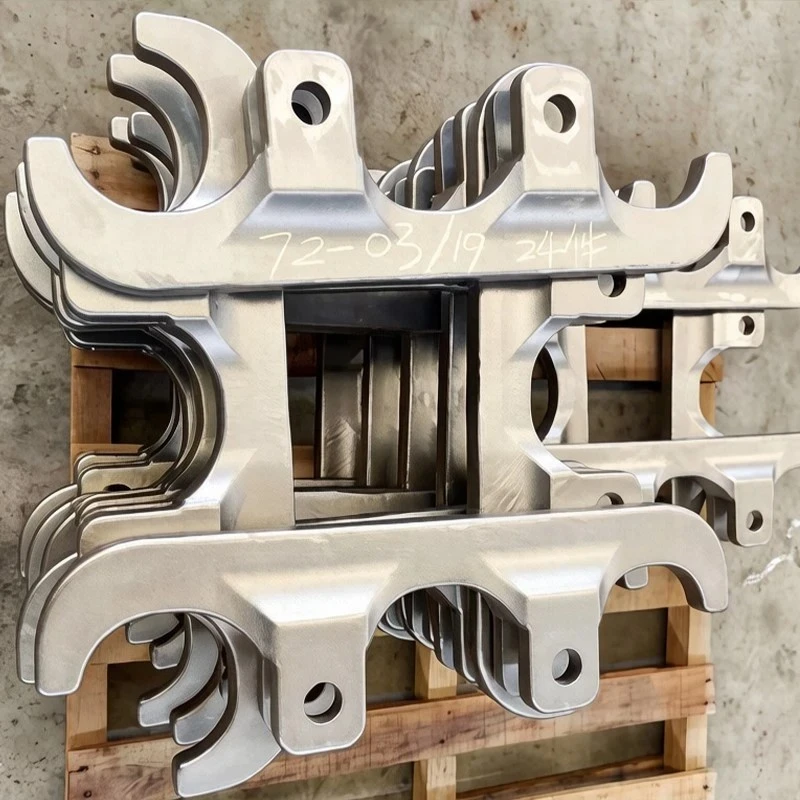
Applications
Crude and Vacuum Process Heaters (CDU/VDU): Supporting horizontal radiant passes along firebox walls and roof arches where tube sagging can kink return bends and cause localized hotspots.
Ethylene Pyrolysis Furnaces: Suspending vertical hairpins and multi-pass cracking tubes subject to rapid, violent thermal expansion between cracking cycles and steam-air decoking.
Continuous Catalytic Reformers & Hydrotreaters: Guiding vertical radiant passes in high-temperature fireboxes while keeping axial growth completely unrestricted.
Emergency Turnaround Replacements: Supplying split, bolt-together replacement hangers that slip around existing tubes without cutting pressure boundaries or dropping coils.
Technical Specifications
|
Design and Casting Standards |
API 560 / ISO 13705, ASTM A297, ASME Section VIII Div. 1 |
|
Primary Cast Alloy Grades |
ASTM A297 Grade HP / HP40 (25Cr-35Ni) for high-temperature radiant fireboxes (service up to 1,050°C) ASTM A297 Grade HK / HK40 (25Cr-20Ni) for standard radiant wall and intermediate guide clips (service up to 950°C) 50Cr-50Ni-Nb (IN-657) for heaters firing high-sulfur or vanadium-bearing heavy fuel oils ASTM A297 Grade HH (25Cr-12Ni) for lower-temperature radiant shield areas |
|
Design Temperature Rule |
Flue gas design temperature plus 100°C (180°F), with a mandatory minimum threshold of 870°C (1,600°F) per API 560 |
|
Corrosion Allowance |
Minimum 1.3 mm (0.05") for austenitic alloys; 2.5 mm (0.1") for ferritic grades |
|
Maximum Unsupported Tube Span |
Strictly limited to 35 times tube outer diameter, never exceeding 6.0 m (20 ft) |
|
Design Load Rating |
Sized for full tube metal weight, flooded liquid inventory, and internal coke deposit allowances |
Customization Capabilities
Tube-Swapping Split Designs: Two-piece pinned or clevis hangers engineered to unbolt and slide out during maintenance without cutting or dropping radiant coils.
Slotted Thermal Guide Shoes: Extended oval slots and sliding saddles machined to handle bidirectional tube growth without binding during rapid startups.
Fuel-Ash Corrosion Metallurgy: Pouring 50Cr-50Ni-Nb (IN-657) alloy for furnaces burning heavy bunker fuel, resisting low-melting vanadium pentoxide (V2O5) ash attack.
Custom Wall-Anchor Matching: Fabricating weld-on casing brackets, ceramic fiber refractory sleeves, and alloy tie-rods matched to your furnace casing steelwork.
Zero MOQ Turnaround Support: From an emergency run of 20 replacement roof hangers to a complete firebox order of 1,200 cast brackets, we pour to order with no minimums.
Quality Control
Full ISO and ASME Shop Credentials: Built under our ISO 9001:2015, ISO 14001:2015, and ISO 3834-2 welding quality systems.
Cast Heat QR Serialization: Every bracket, hanger ear, and pin carries an etched QR code and cast heat number linking directly to spectrographic melt logs and foundry records.
100% Surface Inspection: Liquid Penetrant Testing (PT) across all high-stress fillet radii, pinholes, and critical load-bearing sections to eliminate hot tears and surface porosity.
Proof Load Pulling Tests: Destructive and proof-load mechanical pulls performed on sacrificial casting coupons to verify room-temperature and elevated-temperature tensile strengths.
Export Timber Packing: Heavy wooden crates with internal compartmentalized partitions, rust-preventive coatings on machined pin bores, and desiccant packs for ocean transport.
FAQ
Q: How do you prevent hanger pins from galling and seizing under 900°C flue gas?
A: Pin seizure happens when tight machining tolerances don't account for differential thermal expansion and oxide scale buildup. We machine generous pin-hole clearances per API 560 rules, chamfer pin edges, and cast the mating parts from compatible high-temperature alloys with different hardness values to prevent micro-welding in the firebox.
Q: Can your split hangers really be replaced without cutting into the furnace tubes?
A: Yes. Traditional one-piece cast hangers require cutting the pressure pipe or sliding the entire coil out of the furnace. Our split design uses a two-piece clamp secured by a high-alloy cross-pin. Maintenance crews simply pull the pin, slide the two halves out from behind the tube, and bolt the new bracket in place while disturbing only a few inches of refractory blanket.
Q: What is the typical lead time if our refinery needs replacement hangers during an unplanned shutdown?
A: If we have existing patterns for your hanger size (HK40 or HP40), we can pour, heat-treat, machine, and inspect a batch of replacement castings within 2 to 3 weeks. New patterns typically add 10 to 14 days. Full-furnace production runs usually ship in 8 to 10 weeks.
Q: What commercial and shipping terms do you operate under?
A: We ship under EXW, FOB, or CIF terms via Shanghai or our local Yangtze River terminal. Standard terms are 30% advance deposit, 40% upon NDT/PMI inspection sign-off, and 30% balance prior to ocean dispatch, payable in USD, EUR, or RMB.
Hot Tags: radiant tube support hanger, China radiant tube support hanger manufacturers, suppliers, factory, Cold Wall Manifold, Heat resistant steel tube hanger, Helical Finned Tube, High temperature high pressure cold wall pipe, Spring loaded tube hanger, Thick walled intermediate tube plate


